
Fibrothal Heating System
Customer Application & Background Existing Details: PIT TYPE- GCF —Batch Furnace 90KW Furnace Existing Solution of Fiber Lining & Strip Elements Furnace ID — 1160mm Retort OD- l066mm Total Insulation Lining — 300mm one side Kanthal Solution: Fibrothal – HS Lower shrinkage Less no. of studs as compared to strip and fiber lining Energy savings […]
Customer Application & Background
Existing Details:
- PIT TYPE- GCF —Batch Furnace
- 90KW Furnace
- Existing Solution of Fiber Lining & Strip Elements
- Furnace ID — 1160mm
- Retort OD- l066mm
- Total Insulation Lining — 300mm one side
Kanthal Solution:
- Fibrothal – HS
- Lower shrinkage
- Less no. of studs as compared to strip and fiber lining
- Energy savings and higher production output
Country & Location – Punjab, India
Industry – Tractors – Manufacturing Furnace Type – PIT TYPE FURNACE
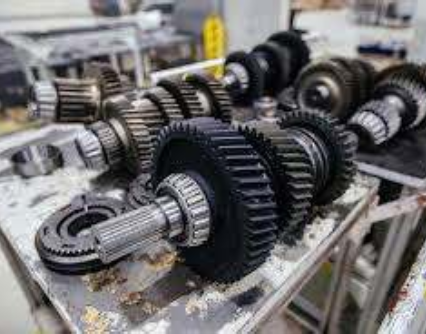
Process – Gas Carburizing of gears
Existing Details:
- Furnace Temperature — 920C
- KW Rating of Furnace — 90KW
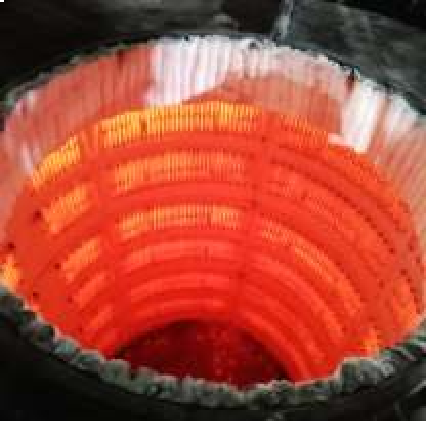
Fibrothal Solution:
- Low thermal mass — skin temperature Around 62 C-65 C (Ambient temperature — 35C)
- Energy savings and higher production output
Electrical consumption difference during initial heating of furnace
| Furnace name |
Insulation | Initial temp. |
Start time |
Stop time |
Time taken |
Initial reading |
Final reading |
Consumption in kW/H |
|---|---|---|---|---|---|---|---|---|
| GCF04 | Strip + Element | 176 | 13.15 | 15.43 | 02.28 | 120766 | 121032 | 266 |
| GCF02 | 100 | 17.25 | 17.25 | 01.10 | 59483 | 59582 | 99 | |
| Difference | 01.18 | 167 |
Electrical consumption difference during continuos load
| Furnace name |
Insulation | Initial temp. |
Final temp. |
Time taken in Hrs. |
Consumption in kW/H |
|---|---|---|---|---|---|
| GCF04 | Strip + Element | 500 | 910 | 2.55 | 446 |
| GCF02 | 500 | 920 | 2.00 | 350 | |
| Difference | 0.55 | 96 |